
HANDMADE AXES SINCE 1902
Our Production
For more than 100 years, Gränsfors Bruk has built up a business around the production of hand forged axes and axe knowledge, with a focus on quality and environmental responsibility.
OUR PRODUCTION PHILOSOPHY
Combining the talents of the blacksmiths at Gränsfors Bruk and designer Hans Erik Persson, Gränsfors Bruk went back to sometimes long-forgotten knowledge to develop a range of axes that are perfect for the small-scale uses of today. The core focus has been on producing axes with sound green credentials, avoiding any unnecessary consumption of natural resources.
All the axes produced by Gränsfors Bruk are forged by hand. Any piecework arrangements have been scrapped so that the smiths can put more time into forging a good axe, removing the need for the excessive post-production work that other manufacturers might use to conceal faults in their forging. This is something that sets Gränsfors Bruk’s axes apart from axes made on an industrial scale. At Gränsfors Bruk, the forging is allowed to take its time.
The axe heads need no grinding, honing or polishing, except on the cutting edge itself, and they certainly do not require painting or varnishing. Instead of using environmentally hazardous epoxy adhesive, the handles are now attached with a traditional wooden wedge, which is better not only for nature but also for the working environment. The sheath supplied with Gränsfors Bruk’s axes is made from vegetable-tanned leather.
Axe production at Gränsfors Bruk is based on five fundamental theses:
An axe is only as good as the accumulated skills of the people who forge, grind and attach the handle to the axe.All our axes are made by human hand. And all these people deserve great respect and recognition for their professional expertise. Our company would be nothing without them.
Smarter production requires fewer natural resources and imbues a product with better quality and a longer life. A longer product life in turn decreases the overall consumption of natural resources and reduces waste.
Every unnecessary step in axe production should be stripped out. Unnecessary grinding, polishing, painting and use of epoxy adhesive for the handle has been eliminated. This makes for a better working environment, lower energy consumption and less of an impact on nature.
We have unlimited responsibility for Total Quality. Working conditions, product quality and concern for nature are just some factors determining Total Quality. Others include humanity, ethics and beauty.
Sound knowledge of a product increases its value and life. The axe user therefore needs information – The Axe Book is one source, courses and Gränsfors Axe Museum are others.
Our production: Step by Step


From Steel to Finished Axe
Our Production
Step 1: Forging
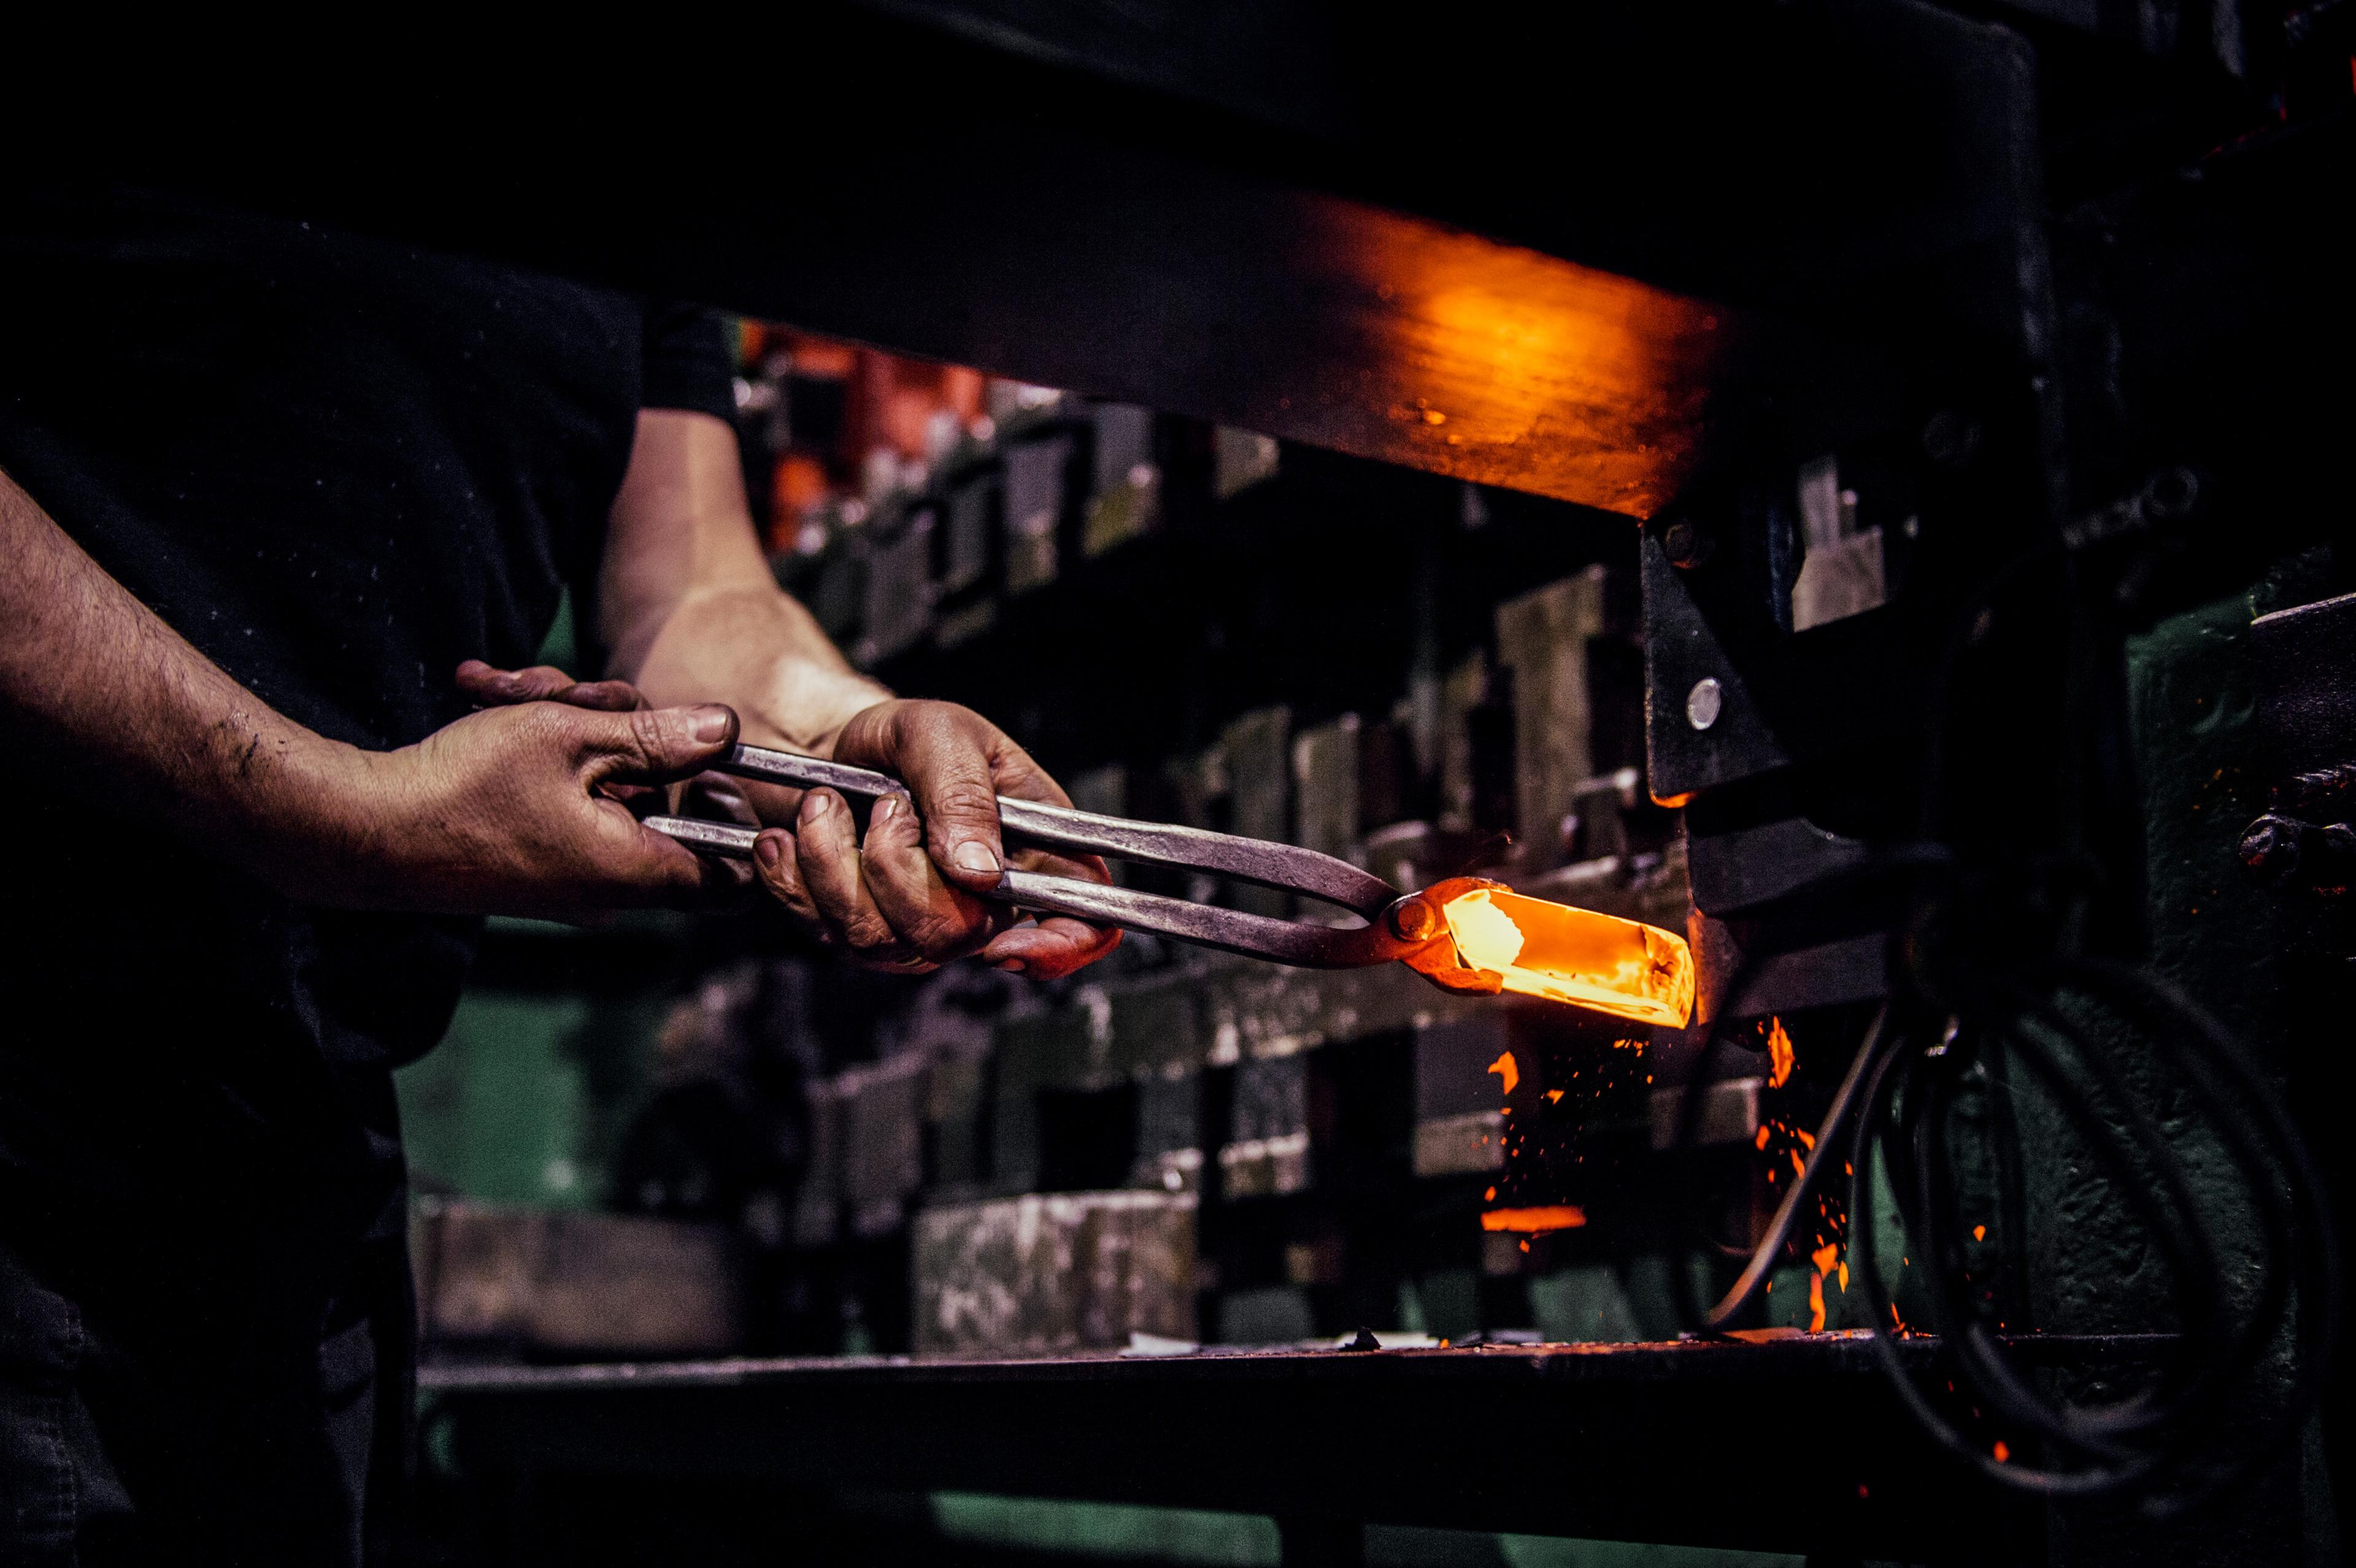
Our axes are made of a special alloy recycled steel with high carbon content. We heat the steel to approximately 1200° C before the blacksmith takes it out of the heat and works it in a large press.
With 80 strikes per minute, the press has a force of approximately 180 tons in each blow. The blacksmith quickly and skillfully handles the hot steel, which transforms slowly from a square of raw material into a finished axe head.
When the steel is treated with great force and repeated blows, the material’s structure is changed. This is why Gränsfors’ axes can be thinner, with a broader edge, and sharper than axes made with just one or a few blows.
The blacksmith finishes their work by stamping Gränsfors Bruk’s label and their initials in the axe head. The initials serve both as a quality seal and to show that there’s a person behind each axe. The blacksmith then hangs the axe head for cooling.
When we forge the axe head, the eye is slightly compressed and can leave a small fold in the material. This is not a defect but rather a natural result of the forging process, and can be found on several of our axe models.
Step 2: Grinding, Hardening & Tempering
After forging, the focus turns to grinding and sharpening the edge. The rest of the axe head is left just as it is. After coarse grinding, the edge is hardened by heating it to 820°C and then rapidly cooling it in water. The hardening makes the steel much harder, but also rather brittle.
To remove the stresses in the steel caused by the forging and hardening, the steel needs to be tempered, which involves keeping the axe heads in an oven at 195°C for 60 minutes. The hardness of the steel depends chiefly on its carbon content, but also on the tempering temperature.
Oil or lead can be used as an alternative to water for cooling. However, Gränsfors Bruk only use water since that is the most eco-friendly option.
Step 3: Tumbling and sharpening
After the grinding, tempering and hardening we tumble the axe head with small ceramic balls to remove any scale left from forging. This tumbling also makes the axe’s surface more rust-resistant.
After tumbling, the steel’s hardness is tested to be sure it is neither too hard nor too soft. Then, the axe’s edge is tested by striking the corner to ensure that there are no cracks in the steel. This whole process ensures that the forging, hardening and tempering were adequately carried out and that the axe has the quality that has become our trademark. Finally, the axe is sharpened and polished to an extremely keen edge.
Step 4: Fitting the axe with a handle
When the axe has been sharpened, we dip the axe head in a water-resistant anti-rust oil. The head is left to dry slightly, then it is time to attach the handle. We fix the handle into the axe head using a pneumatic press and secure it with a wooden wedge.
Gränsfors Bruk’s handles are all made of hickory, an excellent wood for this purpose as it is strong and flexible, with long fibres.
Only our splitting axes feature a small steel wedge. Since these axes are used with greater force, the steel wedge acts as extra security to prevent the axe head from loosening from the handle.
Step 5: Quality Control
All axes undergo several quality control checks before leaving the factory to be absolutely sure that the piece is free from flaws. When the axe passes our quality control, we add a sheath of vegetable-tanned leather to protect the edge and pack it together with the Axe Book.
All Gränsfors Bruk’s axes also carry a 20 Year Warranty*.
(*The Warranty applies as long as the axe is used and cared for properly. The warranty includes the axe head, but not the handle or the leather sheet. See full terms here).

The Blacksmiths initials
The blacksmith finishes their work by stamping Gränsfors Bruk’s label and their initials in the axe head. The initials serve both as a quality seal and to show that there’s a person behind each axe.
BE – Besseling Emiel
EE – Engberg Bohjort Emil
DE – Eriksson Daniel
MF – Forslund Martin
FS – Skoglund Fredrik
MS – Sundberg Mikael
AS – Strömstedt Anders
JW – Wolferen Van Jasper
CÅ – Ångman Charlie
TP – Persson Tobias
EL – Emanuel Larsson
RE – Rickard Eriksson
Blacksmiths mark special products:
 Sam Ritter
 Fabian von Elern
PJA – Alford Paul James
RA – Andersson Rune
TA – Andersson Tomas
KB – Benkwitz Kyle
SB – Beyeler Simon
HD – Danielsson Henrik
LE – Enander Lars
JE – Eriksson Joakim
PE – Eriksson Per
OE – Eliasson Oscar
LF – Faul Lukas
DF – Faxby David
HF – Frank Håkan
DP – Gas Pallarés Domingo
DG – Gräntz Daniel
PH – Hansson Patrik
JMH – Hassel Jessica
MH – Hulin Marcus
JH – Hårdsten John
CK – Kowalek Claudia
AM – Magnusson Anders
YT – Tsegai Yohannes
CM – Malm Christoffer
MM – Mattsson Mattias
LP – Pettersson Lennart
KS – Sjölund Kjell-Åke
TT – Thelin Tobias
TV – Alexander Thomas Viktor Mattsson
BK – Beyene Kahsai
WE – Widarsson Erika
LH – Hejmer Linus
PW – Walldin Per
EB – Blixt Erik
UN – Nilsson Ulrik
JB – Berglund Jonas
MB – Blixt Mattias
CS – Sjölund Christian
RO – Olofsson Roine
TE – Eneroth Tom
IB – Iversen Bryant Joakim
EW – Brhane Weldgergis Eseyas
JL – Lindström Jesper
ES – Sjöström Erik
JS – Johansson Schyberg Stefan
 Ulrika Stridsberg
 Fredrik Thelin
 Hannes Thelin
